In the Czochralski (CZ) process, the continuous rotation of the crystal and crucible is not an auxiliary operation but the “master switch” that determines crystal quality. Rotation systematically ensures the uniformity, integrity, and electrical performance of single‑crystal silicon through six mechanisms: establishing an axisymmetric thermal field, driving forced convection, controlling the solid‑liquid interface morphology, improving dopant uniformity, determining the cylindrical shape, and the synergistic optimisation of crystal and crucible rotation.
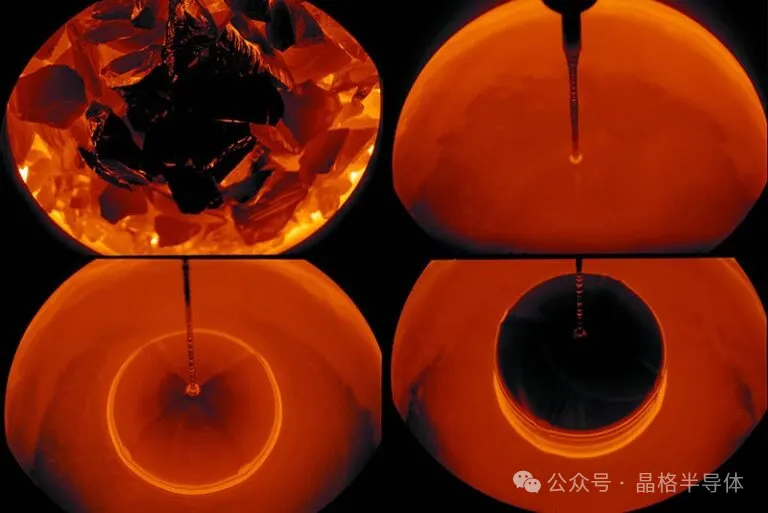
📊 Quick Overview of the Six Mechanisms of Rotation
| No. | Mechanism | Core Principle | Effect on Crystal Quality |
|---|---|---|---|
| 1 | Axisymmetric thermal field | Rotation converts static asymmetric thermal field into dynamic axisymmetric one | Ensures radial uniformity, prevents dislocation multiplication |
| 2 | Forced convection | Suppresses uncontrolled natural convection | Stabilises growth rate, eliminates impurity striations and vortex defects |
| 3 | Interface control | Rotation parameters adjust interface morphology (flat or slightly convex) | Reduces dislocation density, improves crystal integrity |
| 4 | Dopant uniformity | Forced convection improves dopant distribution | Controls resistivity fluctuation (< ±20% or even ±10%) |
| 5 | Cylindrical shape | Rotation‑pull process determines the axisymmetric geometry | Produces round wafers, meeting semiconductor process requirements |
| 6 | Synergy of crystal and crucible rotation | Matching dual‑rotation parameters | Balances thermal field, convection, interface, and doping properties |
❓ Why Is Continuous Rotation Essential in the Czochralski (CZ) Process?
Answer: The Czochralski (CZ) method is the dominant technology for growing single‑crystal silicon, accounting for over 85% of global production. The continuous rotation of both the crystal and the crucible is maintained throughout the entire process. Its necessity is rooted in the six core mechanisms detailed below.
Mechanism 1: Establishing an Axisymmetric Thermal Field – Ensuring Uniform Crystal Growth
The problem: The thermal field inside a CZ puller is extremely complex. Geometric imperfections of the heater, crucible, insulation, and non‑uniform temperature distribution within the melt can all lead to thermal asymmetry. If left uncorrected, such asymmetry can cause radial performance variations, or worse, dislocation multiplication and even crystal fracture.
The role of rotation: Crystal and crucible rotation “smooths out” the thermal asymmetry. Through rotation, the static asymmetric field is transformed into a dynamic axisymmetric one, ensuring that every circumferential position of the crystal experiences the same thermal history.
Data support: Numerical simulations show that increasing the crystal rotation rate significantly improves the asymmetry of the solid‑liquid interface shape. At the same time, increasing the crucible rotation rate improves the temperature distribution in the melt, gradually bringing it toward axial uniformity.
Conclusion: Rotation is the fundamental prerequisite for establishing a proper temperature distribution and ensuring uniform crystal growth.
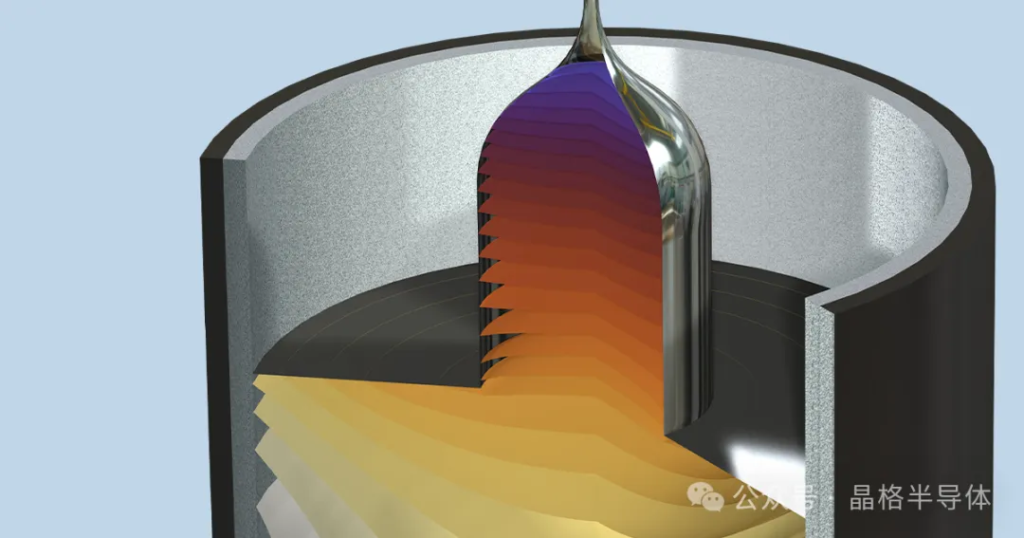
Mechanism 2: Driving Forced Convection – Homogenising Temperature and Composition
The problem: At 1450°C, the silicon melt undergoes strong natural thermal convection driven by buoyancy from temperature gradients. This natural convection is often unstable, causing temperature fluctuations. Studies show that temperature fluctuations near the solid‑liquid interface can exceed 10°C. Such severe fluctuations directly destabilise the growth rate, leading to impurity striations and vortex defects.
The role of rotation: Rotation is introduced to use “forced convection” to suppress uncontrolled “natural convection”. Counter‑rotation of the crystal and crucible induces forced convection – the crystal rotation drives flow beneath the crystal, while the crucible rotation affects the entire melt pattern. Their combined action generates relative motion between the central and peripheral melt zones, creating a relatively stable region just below the solid‑liquid interface.
Conclusion: The direct benefit of forced convection is the homogenisation of temperature and composition, providing a stable liquid environment for high‑quality growth.
Mechanism 3: Controlling Solid‑Liquid Interface Morphology – Reducing Dislocation Density
The problem: The morphology of the solid‑liquid interface (the growth front) directly determines crystal integrity and uniformity. Studies indicate that the interface shape affects dislocation density and the radial resistivity profile. The ideal interface is flat or slightly convex toward the melt; excessive convexity or concavity introduces defects.
The role of rotation: Rotation parameters are the key means of controlling interface morphology. When both crystal and crucible rotation are applied, adjusting their speed ratio yields a flat interface. A flat interface is the key to obtaining low dislocation density and high uniformity.
Additional effect: Within a certain range, increasing crystal rotation rate raises the interface position, meaning that rotation can actively control interface location and thus optimise the thermodynamic conditions for growth.
Conclusion: Reasonable matching of crystal and crucible rotation ratios is a core process measure for achieving a flat interface and lowering dislocation density.
Mechanism 4: Improving Dopant Uniformity – Ensuring Resistivity Consistency
The problem: For semiconductor applications, uniform dopant distribution is critical. Typical requirements are resistivity variation within ±20%; stringent devices demand within ±15% or even ±10%. However, due to dopant segregation, insufficient melt stirring leads to significant axial and radial resistivity differences.
The role of rotation: Rotation, via forced convection, significantly improves the distribution homogeneity of dopants in the melt. Crystal rotation directly affects dopant incorporation and cross‑sectional uniformity, enhancing radial dopant uniformity. Studies show that adjusting crystal and crucible rotation rates can effectively improve the resistivity uniformity of CZ silicon.
Double‑edged effect: The influence of rotation on impurities must be considered carefully. For oxygen, for example, the melt convection modes – including Taylor‑Proudman vortices and buoyancy‑thermocapillary vortices – play different roles in oxygen evaporation and transport. Increasing crucible rotation suppresses certain convection modes, thus affecting the final oxygen content. Therefore, finding the optimal rotation parameter combination is a core process task for balancing all performance metrics.
Conclusion: Rotation is key to improving dopant uniformity and ensuring resistivity consistency, but its effects on different impurities must be carefully balanced.
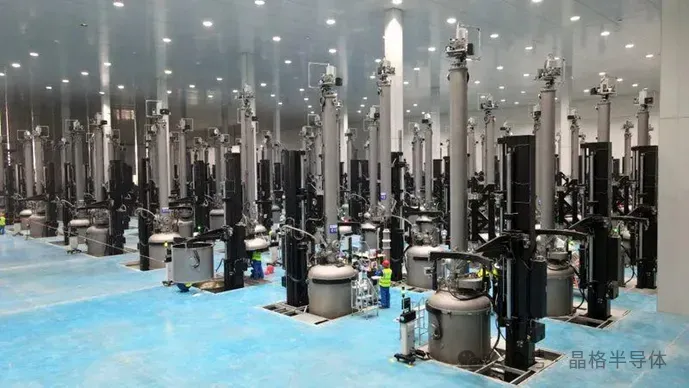
Mechanism 5: Determining the Cylindrical Shape
An intuitive fact: The cylindrical shape of a single‑crystal silicon ingot is determined precisely by the rotation‑pull process. In the CZ method, the seed crystal is rotated while being pulled upward, and the molten silicon grows along the seed orientation into a cylinder. By precisely controlling rotation and pulling speeds, the crystal diameter can be adjusted to meet the requirements of necking, shoulder, and constant‑diameter growth stages.
Counter‑argument: Without rotation, the crystal would not acquire an axisymmetric geometry, and the subsequent wafers would lose the circular shape that is essential in semiconductor manufacturing.
Conclusion: Rotation directly determines the macroscopic shape of the crystal and is the physical prerequisite for obtaining round wafers.
Mechanism 6: Synergistic Optimisation of Crystal and Crucible Rotation
Division of labour and synergy:
| Rotation Type | Main Affected Region | Core Function |
|---|---|---|
| Crystal rotation | Near the solid‑liquid interface | Determines micro‑growth environment and interface morphology |
| Crucible rotation | Entire melt in crucible | Affects macro thermal field and impurity transport |
Synergistic effects: Studies show that appropriate crucible rotation effectively suppresses convection caused by crystal rotation and buoyancy convection, while increasing crystal rotation makes isotherms near the interface flatter. Proper matching of the two suppresses temperature fluctuations near the interface.
Recommended parameters:
- Some studies indicate that the best quality is achieved at crystal rotation = 10 rpm, crucible rotation = –5 rpm (the negative sign indicating counter‑rotation).
- In production, crystal rotation is typically 1–3 times faster than crucible rotation.
- The optimal parameters vary with crystal diameter, thermal field configuration, dopant type, etc. , and require optimisation through numerical simulation combined with experimentation.
Conclusion: Synergistic optimisation of crystal and crucible rotation is a system‑level task that requires careful tuning on a case‑by‑case basis.
💎 Summary
The six mechanisms of continuous rotation in single‑crystal silicon growth can be summarised in the following logical chain:
| Level | Mechanism | Ultimate Goal |
|---|---|---|
| Thermal field | Establish axisymmetric thermal field | Ensure uniform crystal growth |
| Fluid dynamics | Drive forced convection | Homogenise temperature and composition |
| Interface | Control solid‑liquid interface morphology | Reduce dislocation density |
| Doping | Improve dopant uniformity | Ensure resistivity consistency |
| Shape | Determine cylindrical shape | Obtain round wafers |
| Synergy | Optimise matching of crystal and crucible rotation | Balance all performance indicators comprehensively |
Core logic: Continuous rotation acts on five independent dimensions – thermal field, fluid, interface, doping, and shape – and achieves global optimisation through the synergy of crystal and crucible rotation: five‑dimension synergy, integrated optimisation.
Final conclusion: The continuous rotation of crystal and crucible in the CZ method is by no means a dispensable auxiliary operation. It is a core technical means that systematically safeguards crystal quality throughout the entire growth process. Understanding and optimising these six mechanisms is the prerequisite for growing high‑quality single‑crystal silicon.
Article source: Jingge Semiconductor — Supplies ultra‑large‑size single‑crystal silicon materials and polycrystalline columnar‑grained silicon materials. Our products are specifically designed for the processing of silicon components used in semiconductor etching applications, including single‑crystal silicon rings, single‑crystal silicon wafers, columnar‑grained silicon rings, and polycrystalline silicon wafers, with diameters up to 650 mm.